
Engineering the Card and Display Together
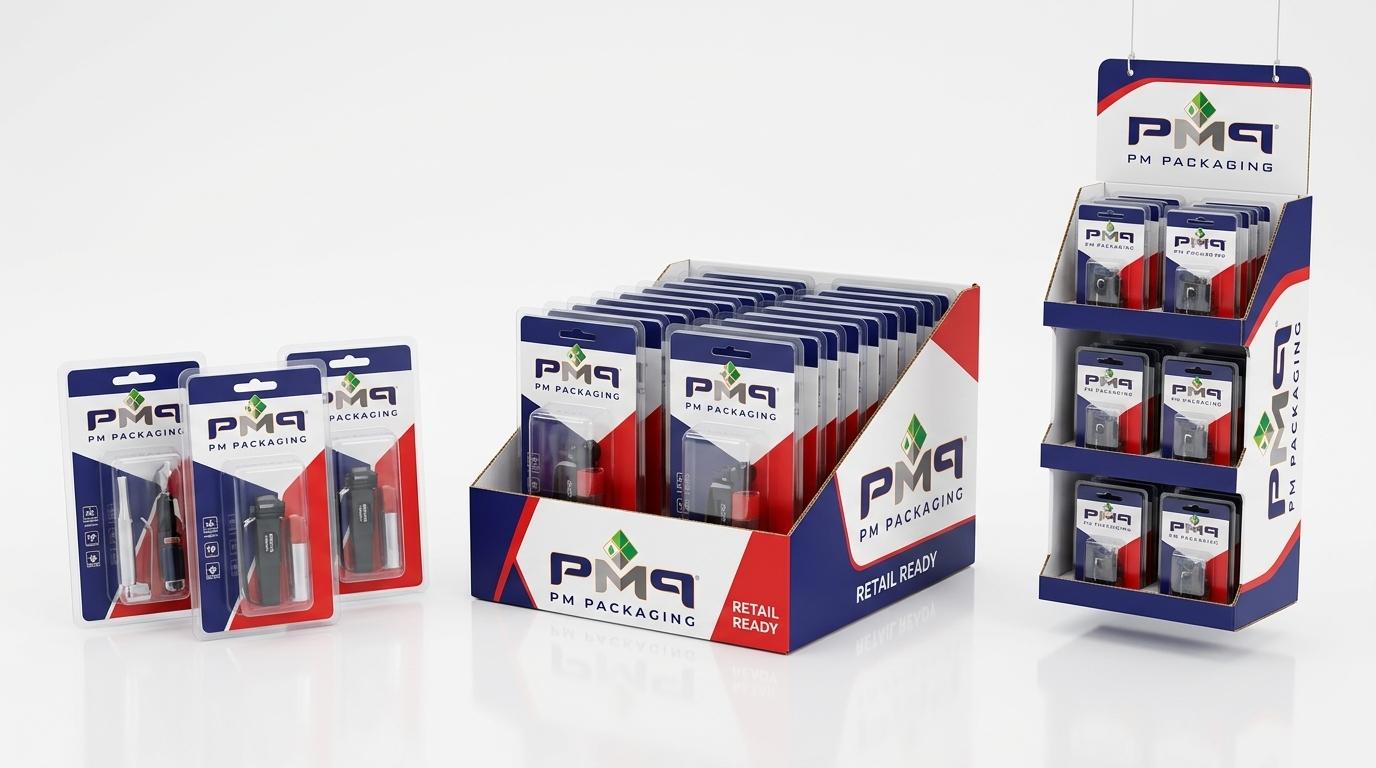
Blister cards and retail displays should be engineered together rather than as separate packaging components. Card width, hang-hole position, product weight, header graphics, peg spacing, tray-wall height, and display capacity all affect whether the final merchandising system works at retail. Coordinating these variables early reduces display-fit problems, improves brand visibility, and simplifies pack-out for larger retail programs.
Design the Blister Card and Display as One Retail System
When brand teams develop the primary blister card first and postpone display engineering until launch, severe structural conflicts emerge. A card that is just 1/4-inch too wide can force a counter tray from four product facings down to three, forfeiting 25% of retail shelf capacity. Similarly, neglecting the 3D depth of the thermoformed plastic cavity causes cards to bind together or flop forward. Designing the card and display simultaneously guarantees that dimensions, weight distribution, and graphics align on retail sales floors.
Start With the Retail Merchandising Format
The physical destination of your product dictates how your blister card must be engineered. Different retail display formats place contrasting mechanical and visual demands on paperboard packaging:
Standard Pegboard Fixtures
Cards hang from store peg hooks. Demands precise hang-hole centring, proper paperboard caliper (20pt–24pt SBS), and balanced product center of gravity to prevent tilting.
PDQ Counter Trays
Cards sit upright in gravity-fed corrugated trays. Requires calibrated front-lip height, lean-back rake angles, and internal guide lanes to keep cards standing neatly.
Sidekicks & Power Wings
Hanging perimeter displays on endcaps. Demands strict overall width limits (14"–16"), shallow depth profiles, and secure hook attachments under shopper traffic.
Multi-Tier Floor Stands
High-capacity promotional displays using peg panels or shelves. Demands disciplined vertical load distribution to prevent top-heavy tipping and structural bowing.
Whether your retail program calls for in-store displays assembled in-store or turnkey prepacked shippers, establishing the merchandising fixture upfront sets the engineering constraints for every dieline decision.
Standardize Blister-Card Dimensions Across SKUs
When a product family encompasses multiple variations—such as different tool sizes, cosmetic shades, or accessories—creating bespoke card sizes for each item causes display chaos. Standardizing card footprints across your SKU family creates a shared merchandising grid. Keeping backing card widths and heights uniform allows a single floor stand or counter tray to merchandise any combination of SKUs without custom internal partitions, while aligning brand headers into a clean, cohesive billboard.
Coordinate Peg Spacing and Hang-Hole Position
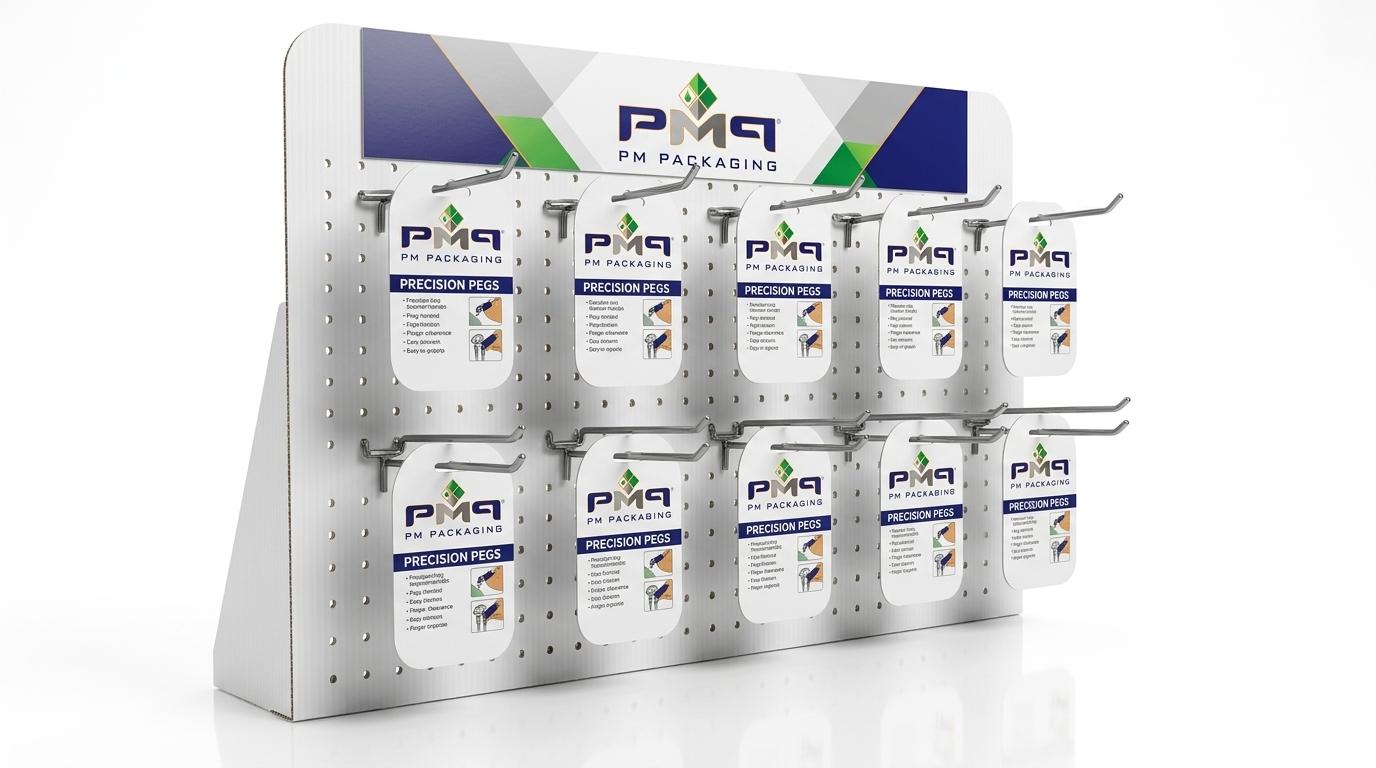
On pegged displays, proper peg spacing requires exact mathematical discipline:
- Horizontal Peg Pitch: Calculated as Card Width + 0.50" to 0.75" Finger Clearance. Placing hooks exactly card-width apart causes packages to overlap, curling paperboard edges and making removal frustrating for shoppers.
- Vertical Clearance and Lift Allowance: Calculated as Card Height + 1.50" to 2.00" Lift Margin. Shoppers must lift a card over the curved tip of a wire hook. Without this overhead margin, consumers bend the paperboard or tear the hang hole against the row above.
- Hang-Hole Tear Strength: Dense products require 20pt to 24pt SBS paperboard or reinforced sombrero tabs to resist tearing under customer handling. To explore hang-hole balance dynamics, read our guide on How Card Size Affects Blister Packaging Performance.
Account for Product Weight and Center of Gravity
When a dense item is placed in a deep thermoformed cavity, the center of gravity shifts forward, pulling away from the backing card plane. On peg hooks, an unbalanced center of gravity causes cards to tip downward, misaligning branding and pulling forward on the display panel. On multi-tier floor stands, grouping heavier products on the lowest hooks or shelves anchors the base, lowering the fixture's center of gravity to prevent tipping under customer traffic.
Design Counter Displays Around Card Visibility
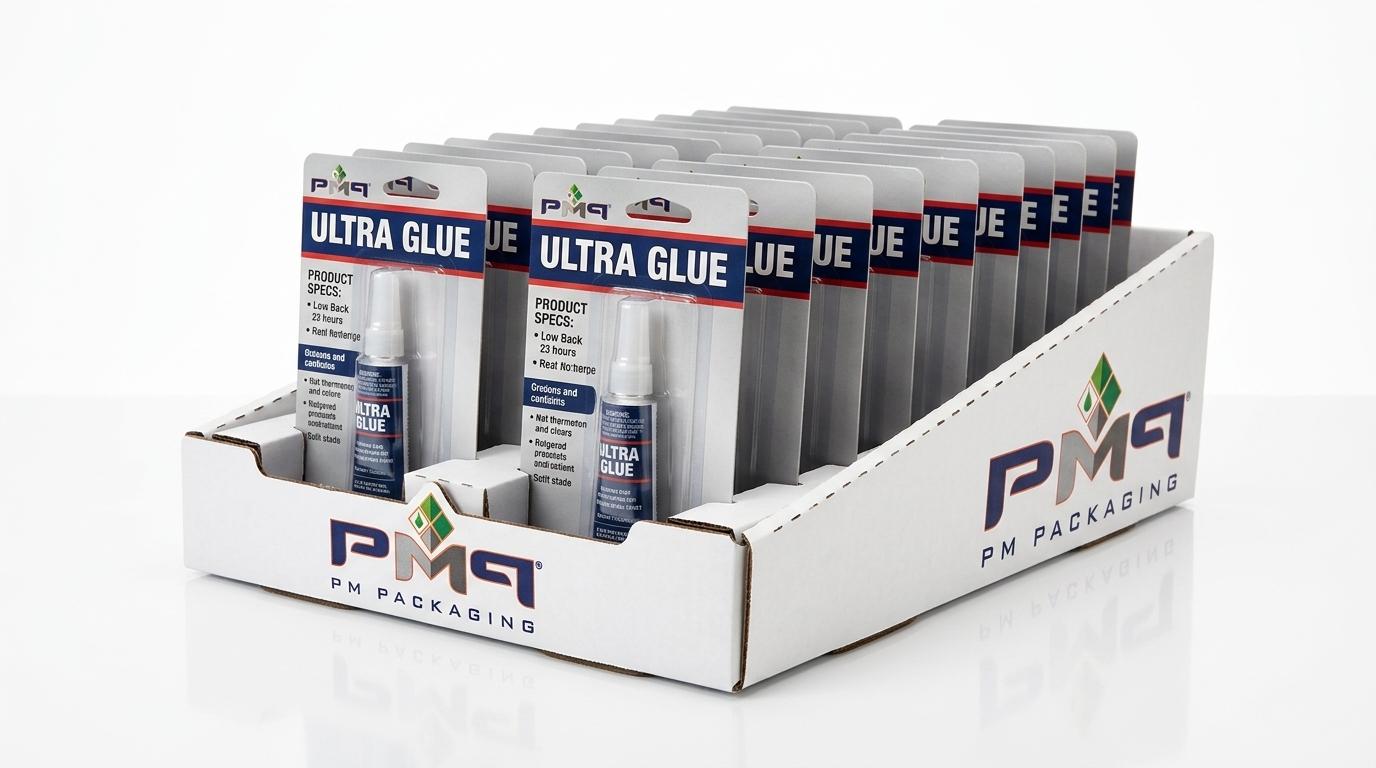
Counter PDQ trays drive checkout impulse sales, but require specific structural considerations:
Front-Lip Height Calibration
An overly tall front lip obscures product branding and cavity visibility, while a shallow lip allows cards to tumble forward. Calibrate the front lip to the minimum height necessary to retain the card base.
Lean-Back Rake Angle (3° to 5°)
When partially sold down, freestanding cards slump forward. An engineered 3-to-5 degree backward slope in the tray floor uses gravity to keep remaining cards standing upright.
Anti-Shingle Guide Rails
Internal dividers or lane guides prevent cards from sliding diagonally (“shingling”), keeping all facings square to shoppers. For checkout strategies, see How Blister Cards Support Impulse Purchases.
Plan Floor Displays Around Load Distribution
Floor displays must withstand weeks of shopper traffic without sagging. Placing heavy SKUs on upper peg rows creates a top-heavy lever arm that bows corrugated back panels forward and loosens base tabs. Grouping heavier products on lower hooks and lighter SKUs above preserves structural column strength and ensures long-term promotional stability.
Coordinate Graphics Between the Card and Display
Graphic harmony between packaging and display reinforces brand authority:
- Hierarchy of Messaging: Use display headers and side panels for high-level campaign slogans and brand positioning, reserving the blister card for product specifications and model identification.
- Background Contrast: Avoid matching display back-panel colors identically to blister card backgrounds. If both are dark blue, individual products disappear. A contrasting backdrop makes individual cards pop.
- Cross-Substrate Color Matching: SBS paperboard cards and corrugated litho-laminate (SFL) displays absorb ink differently. Managing production under G7 standards ensures consistent brand colors across formats.
Engineer Prepacked Displays for Distribution
Prepacked display shippers eliminate in-store assembly labor by arriving 100% stocked and ready to merchandise. However, prepacks must survive freight transit. Road vibration can cause suspended cards to bounce off peg hooks, damaging paperboard edges and scuffing plastic bubbles.
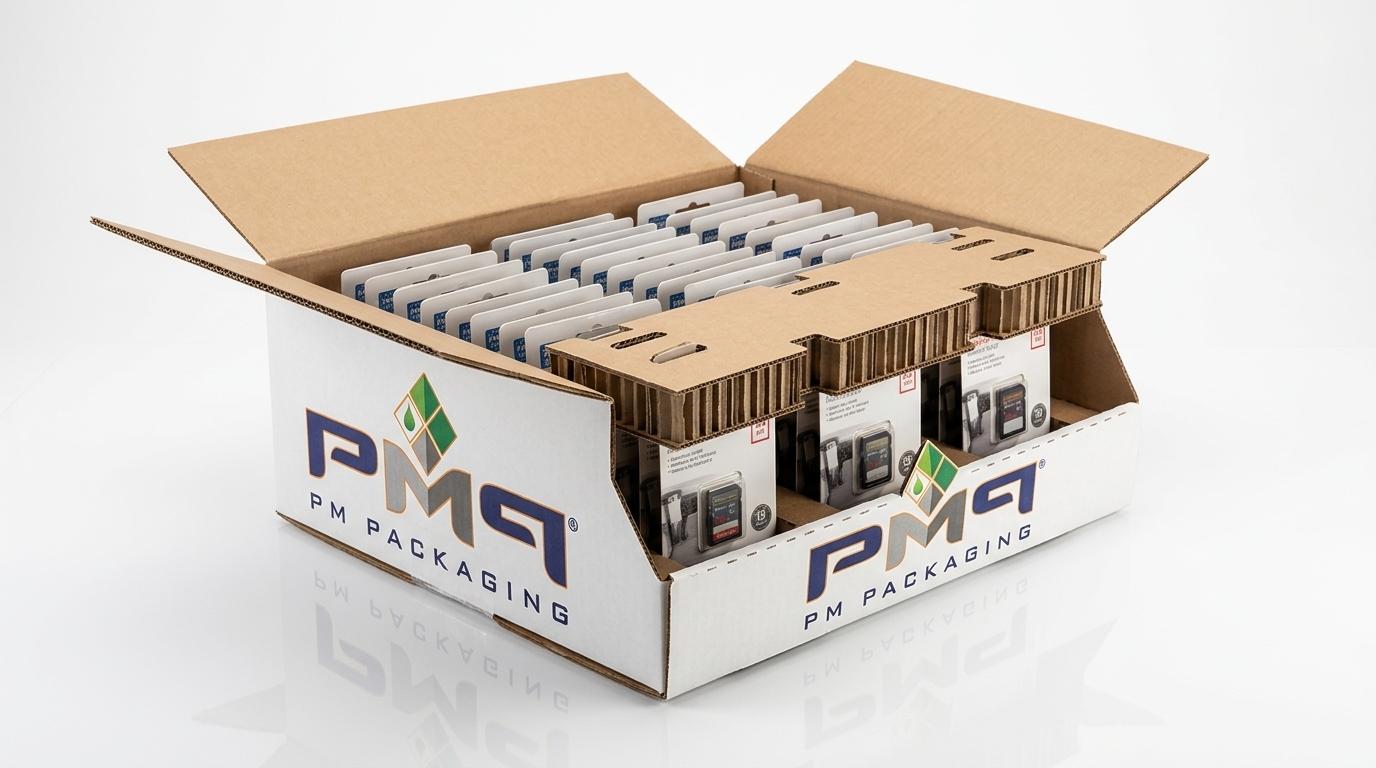
Protecting prepacks requires custom die-cut corrugated locking bars or foam inserts that slide over peg hooks to immobilize cards during transit. Combined with heavy-duty outer master cartons, retail staff simply remove the outer shipper and slide out the locking bar—achieving instant merchandising compliance in seconds.
Coordinate Display Capacity With SKU Velocity
Allocating equal display capacity across all SKUs invites stock-outs. If an 8-SKU display gives equal space to every variant, top-selling items stock out within 48 hours while slower-moving items linger. Aligning facings and hook depths with actual sell-through velocity balances inventory depletion rates and reduces store restocking frequency.
Common Problems When Blister Cards and Displays Are Designed Separately
Designing packaging and displays in isolation routinely generates avoidable retail failures:
Cards Wider Than Peg Spacing
Backing cards overlap horizontally, curling paperboard edges and binding adjacent packages.
Blister Cavity Collision
Plastic bubbles hit neighboring cards, preventing packages from hanging flat.
Tray Walls Obscuring Branding
Tall PDQ lips hide product names, destroying retail visibility at checkout.
Top-Heavy Display Tipping
Heavy items on upper tiers create an unstable center of gravity, risking fixture collapse.
Hang-Hole Incompatibility
Holes misaligned with hook types, causing cards to hang crooked or tear off.
Cards Dislodging in Transit
Cards bouncing off hooks during shipment because transit locking inserts were omitted.
Capacity vs. Velocity Mismatch
Fast sellers stocking out while slow-moving variants tie up display space.
Substrate Color Discordance
Mismatched ink appearances between coated cards and corrugated display structures.
Pallet Cube Inefficiencies
Displays designed with overhangs that violate retail DC distribution guidelines.
When It Makes Sense to Source Blister Cards and Displays Together
Splitting your program between a card printer and a separate display converter introduces administrative handoffs and dimensional discrepancies. Consolidating production with a single manufacturer provides unified CAD dieline modeling, synchronized press schedules, and certified G7 color consistency across both substrates.
To evaluate supplier qualification frameworks for national rollouts, consult our guide on How to Choose a Packaging Partner for a National Retail Rollout and explore our Custom Blister Card Programs for National Retail.
Blister Card and Retail Display Coordination Checklist
Verify critical engineering parameters across primary retail display formats:
| Display Format | Blister-Card Design Consideration | Display Design Consideration |
|---|---|---|
| Counter / PDQ tray | Card width, header visibility, card stiffness (20pt+ board). | Tray wall height, lane width, product count, 3°–5° lean-back angle. |
| Pegged floor display | Hang-hole position, card weight, product center of gravity. | Peg spacing (0.50"–0.75" gap), hook length, lift clearance, display stability. |
| Sidekick / power wing | Compact card dimensions, hanging durability, shallow cavity depth. | Overall width (14"–16"), attachment system, weight distribution. |
| Multi-tier floor stand | Product orientation, SKU differentiation, consistent footprint. | Shelf spacing, load distribution, heavy items low, replenishment access. |
Coordinate Your Retail Packaging Program With PM Packaging
Planning a blister-card program with counter, PDQ or floor displays? PM Packaging can help coordinate card dimensions, display structure, graphics, pack-out and shipping requirements as one retail packaging system.
Explore our end-to-end manufacturing and packaging programs for procurement and supply chain teams. Connect with our structural design engineers to review dielines and develop production-intent prototypes.