
How to Determine the Right Blister-Card Dimensions
The right blister-card size is the smallest practical footprint that still provides enough room for the blister cavity and sealing flange, required branding and technical information, a structurally sound hang area, and the retailer’s planogram requirements. Card width affects peg density, card height affects header visibility and vertical clearance, and blister depth affects hook capacity, hanging stress, and shipping cube. Product weight, pack-out equipment, case packs, and SKU standardization should also influence the final dimensions.
Start With the Product—but Don't Size the Card to the Product Alone
A common mistake in packaging development is treating a blister card as a simple rectangle slightly larger than the physical product. When a brand has an item measuring 2 inches wide by 3 inches tall, intuitive guesswork often leads to selecting a 2.5 × 3.5-inch card. In production, that package almost always fails.
A blister card is not just an underlay for an object; it is a structural platform that must satisfy multiple physical, graphic, and mechanical demands simultaneously. Every square inch of the paperboard card must be allocated to specific functional zones:
Cavity & Flange Geometry
Room for the thermoformed plastic pocket plus an unbroken perimeter heat-seal flange bonded to the card substrate.
Header Brand Area
Dedicated vertical billboard space above the cavity for the primary logo, product title, and category signpost.
Hanging Physics & Margins
A standardized euro or delta hang slot positioned with sufficient top-edge paperboard margin to resist tear-out.
Structural Perimeter Margins
Safe distances between the blister flange edge and the card dieline border to prevent die-cutting misalignments.
Regulatory & Machine Code Data
Clean, unencumbered space for scannable UPC/GTIN barcodes, regulatory certifications, country of origin, and batch tracking.
Retail Fixture Clearance
Exact dimensional alignment with retailer pegboard pitch, shelf-to-shelf clearances, and planogram width allocations.
When you account for the thermoformed pocket clearance, perimeter sealing flange, header graphics, hang-hole structure, and back-panel instructions, the physical envelope expands well beyond the object's bare dimensions. The engineering goal is to calculate the precise boundary where every technical requirement is satisfied without adding wasteful, unmonetized paperboard surface.
The Visible Blister Cavity Is Not the Full Blister Footprint
Packaging buyers new to carded packaging often overlook the distinction between the formed blister pocket and the finished blister footprint. The structural chain follows four progressive stages:
The blister cavity encloses and cushions the merchandise, but it is the continuous flat perimeter lip—the sealing flange—that actually bonds the plastic to the heat-seal coated paperboard. Sealing equipment requires adequate surface contact area to apply uniform pressure and heat without crushing the thermoformed sidewall.
If backing cards are sized too tightly around visible cavities, the sealing flange is forced to run directly against the card border. This leaves zero tolerance for rotary sealing registration or tray placement. Under retail handling or warehouse vibration, cards with compromised flange margins experience edge lifting, localized seal separation, and premature package failure.
Card Width Determines How Much Retail Space Each SKU Consumes
In retail merchandising, card width is the single greatest determinant of planogram economics. Retailers measure shelf productivity in revenue and margin per square foot and per linear inch of display fixture. A blister card that is 1 inch wider than necessary directly reduces the number of facings that can hang across a standard 36- or 48-inch display pegboard.
Illustrative Planogram Density Comparison
As an illustrative example, consider a retail peg run spanning 36 inches of horizontal pegboard space (actual hook counts depend on retailer-specific spacing rules and prong clearance):
- •4.0-inch wide card: Illustratively fits up to 8 peg hook columns under common spacing assumptions.
- •5.0-inch wide card: Fits approximately 6 peg hook columns across that same 36-inch section.
In this scenario, widening the card by 1 inch can reduce facing capacity by around 25%, illustrating why retail category managers scrutinize package width during line reviews.
Designing card width involves a strategic trade-off:
- Wider Cards: Provide greater billboard space for multi-item accessory sets, horizontal product arrangements, prominent feature callouts, and multi-language copy blocks. However, they reduce peg density and increase paperboard substrate expenditure.
- Narrower Cards: Maximize facing density, allow retailers to list more SKUs across the fixture, and reduce unit material cost. However, they demand tightly disciplined graphic layout and leave less room for expansive instructional text.
Card Height Affects Header Visibility and Peg Presentation
While card width determines horizontal shelf allocation, card height governs vertical fixture clearances and how packages interact when hung sequentially on peg hooks.
In typical retail aisles, blister cards hang one behind another on 6-, 8-, 10-, or 12-inch metal peg hooks. As shoppers approach the aisle, their line of sight captures the upper brand header of the front card. When customers remove the front unit, the header of the secondary package immediately establishes brand identity.
If a card is engineered too short relative to its blister cavity projection, the blister pocket of the trailing package overlaps and conceals the brand graphics of the package behind it. Conversely, if a card is made excessively tall, it collides with the shelf or peg row above and below it. Store personnel faced with oversized cards are often forced to move peg hooks further apart vertically, reducing total shelf capacity or relegating the product to awkward bottom racks.
For an in-depth guide on optimizing the upper portion of your card dieline, explore our technical breakdown on How to Design the Header Area of a Blister Card.
Card Size, Product Position, and Hang-Hole Placement Work Together
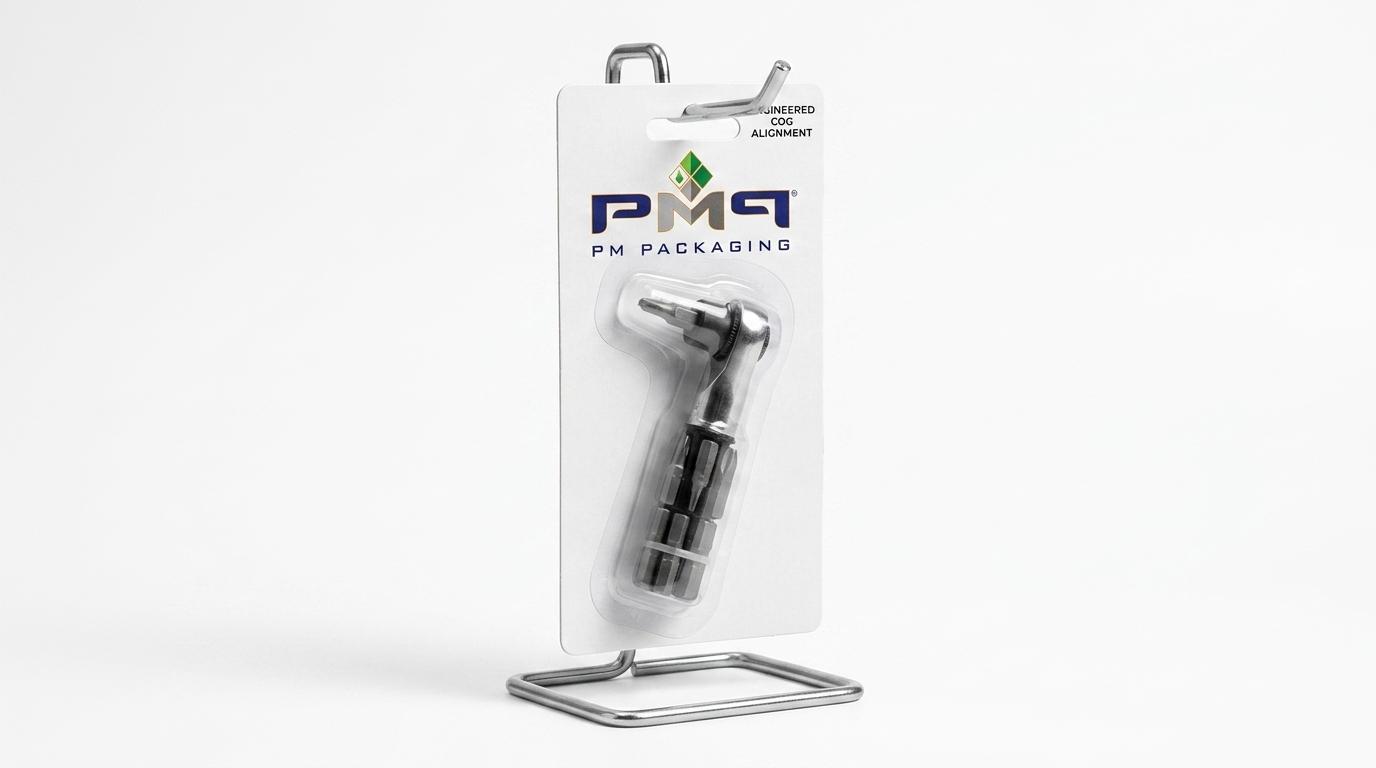
One of the most frequent structural defects seen on retail pegboards is package skew—blister cards hanging at awkward angles rather than plumb and level. This flaw stems from a fundamental misunderstanding of hanging physics:
"Centering a hang hole on the geometric centerline of a card only produces a level package if the product's center of mass is perfectly symmetrical. For asymmetrical items, the hang hole must be engineered directly over the combined center of gravity."
When packaging an asymmetric hand tool, ratchet, faucet assembly, or multi-component kit, the heavier metal mass is often concentrated toward one side or toward the bottom. If the dieline engineer punches a standard euro or sombrero slot at the exact 50% width mark of the card, gravity will pull the heavy side downward, rotating the entire package on the hook.
Crooked packages degrade shelf presentation, disrupt brand blocking across neighboring pegs, and snag on adjacent packages when customers try to pull an item off the fixture. During dieline development, structural engineers must calculate the composite center of gravity (the combined mass of the paperboard card, thermoformed blister, and enclosed merchandise) and align the suspension vertex of the hang slot directly above that vector.
Furthermore, card size dictates hang-hole tear resistance. There must be adequate paperboard margin between the top apex of the hang slot and the upper cut edge of the card. If a card is compressed too tightly vertically, this top margin shrinks. When shoppers browse and slide heavy packages across wire hooks, an under-margined hang slot quickly tears through, rendering the package unsellable on standard pegboards.
Why Paperboard Grain Direction Matters on Larger Blister Cards
Card dimensions cannot be engineered in isolation from substrate properties. As a blister card increases in surface area, it becomes exponentially more vulnerable to cantilever bending and environmental curling.
During papermaking, cellulose fibers naturally align along the direction of machine travel. This creates distinct physical characteristics between the Machine Direction (MD) and the Cross Direction (CD):
- Machine Direction (With Grain): Displays substantially higher stiffness, tensile strength, and resistance to bending under downward or cantilevered mechanical loads.
- Cross Direction (Across Grain): Displays greater flexibility and is more susceptible to deflection when weight is suspended outward from the surface.
On medium and tall blister cards, grain direction should be evaluated as part of the structural specification. Orienting the paperboard grain vertically (parallel to the height of the card) typically provides greater resistance against the forward-leaning cantilever moment of heavier products or deeper blister pockets.
When a tall card is produced with the grain running horizontally across the card width, it can be more susceptible to forward bowing on peg hooks under heavy loads or humidity fluctuations. Because paperboard responds to ambient moisture changes differently across its grain than along it, pairing the right caliper with favorable grain orientation helps keep cards flatter across typical distribution and retail conditions.
Blister Depth Is a Third Dimension of the Retail Footprint
Packaging teams frequently evaluate blister cards in two dimensions on a CAD flat layout (width × height). However, retail space and logistics efficiency are strictly three-dimensional environments. The depth of the thermoformed blister cavity plays an equal role in package performance.
Blister cavity depth dictates:
Peg Capacity & Facing Density
As an illustrative example on an 8-inch peg hook, a package with a 1.25-inch blister depth might hold around 5 to 6 units per hook, whereas increasing cavity depth to 2.5 inches can cut that holding capacity roughly in half, affecting restocking frequency.
Lever Arm & Cantilever Stress
The further a heavy product projects outward from the card face, the greater the rotational torque applied to the upper hang hole and the paperboard substrate, accelerating card creep and sag.
Thermoform Draw Ratio & Wall Thickness
Deeper cavities require greater plastic sheet draw, stretching the polymer and thinning corner radiuses. Controlling depth preserves material rigidity and optical clarity across the pocket corners.
Master Shipper Cubing Efficiency
Unnecessary cavity depth creates trapped air inside shipping cartons, inflating freight volume metrics and reducing the number of units that fit on an outbound shipping pallet.
Don't Size the Cavity Directly to Nominal Product Dimensions
In precision manufacturing, nominal dimensions represent the ideal target, not the physical reality of mass-produced goods. Injection-molded plastics shrink and expand with resin batch variations; stamped metal brackets exhibit slight tooling burrs; rubberized tool grips vary in durometer and thickness; and wrapped cables have unpredictable coil spring-back.
If a thermoforming tooling engineer machines a blister pocket to the exact theoretical CAD dimensions of the product, packing line operators will struggle to seat the merchandise into the cavity. Forcing parts into tight cavities slows cycle times, scuffs product finishes, and can cause the plastic flange to buckle during heat sealing.
Rather than relying on rigid clearance formulas, cavity dimensions should be developed around actual production samples, manufacturing tolerances, and retention needs. Incorporating calibrated clearances around contours allows smooth insertion on the packing line, while selective retention features or contour fits keep the product oriented properly for retail display without binding or rattling.
Dimensional Breakpoints: How Card Dimensions Affect Case Packs and Pallets
The impact of blister-card dimensions extends far beyond the retail shelf into master carton pack-out and freight logistics. In supply chain engineering, packages are subject to dimensional breakpoints—critical thresholds where a fraction of an inch dictates whether a master carton can accommodate an extra row of product.
For example, shaving a fraction of an inch off card width or height may seem minor on an individual unit, but across a 12- or 24-count master shipper, those fractional differences multiply. Small adjustments can help master cartons fit standard 40 × 48-inch North American pallet footprints without edge overhang, reducing the risk of transit damage and improving cube utilization.
Furthermore, secondary packaging efficiency depends on how blister cards are packed inside the master shipper. Depending on product geometry and blister layout, some packages can take advantage of head-to-foot alternating nesting:
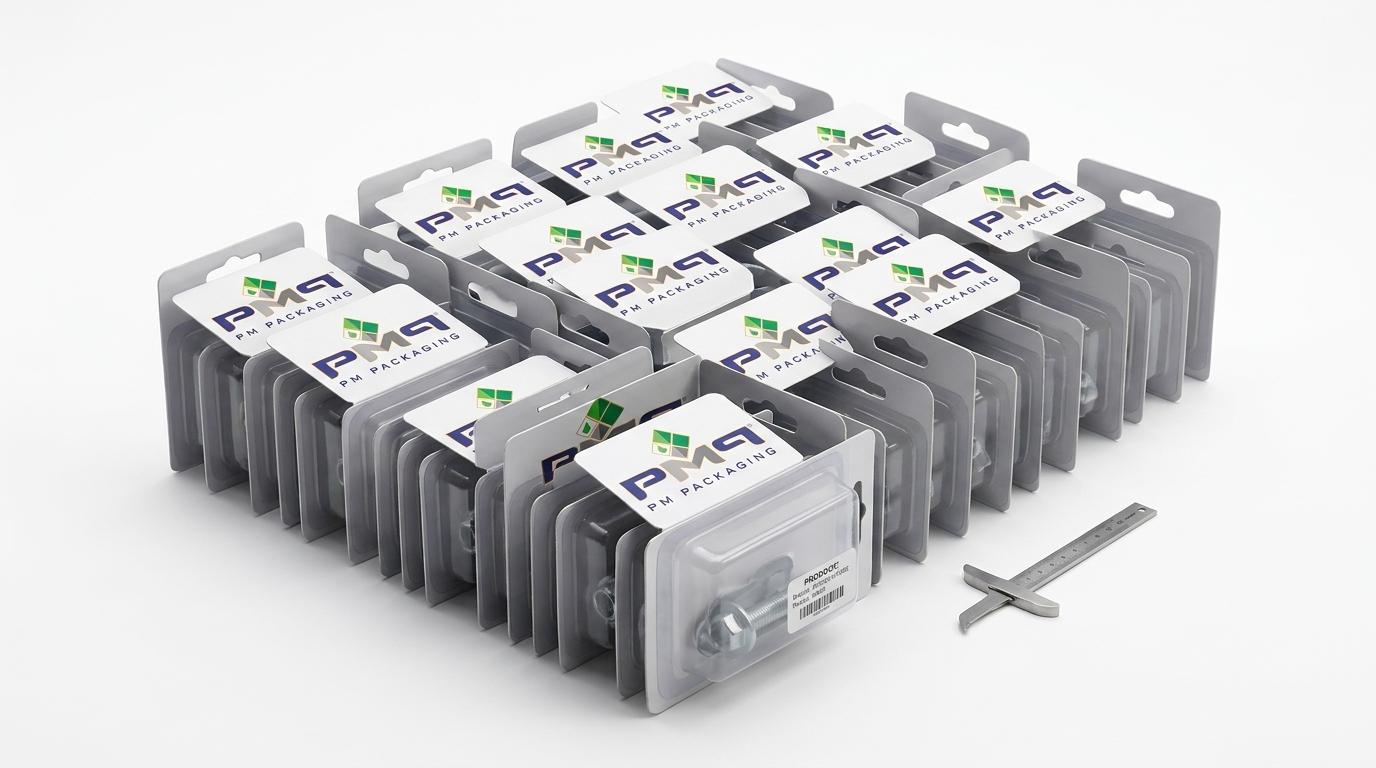
When blister packages are packed facing the same direction, every unit stacks blister-to-back, leaving void space behind each header. When geometry allows staggering cards head-to-foot, the protruding cavity of one package can nest against the flat header area of the adjacent package. This arrangement can materially reduce unused void space in some package configurations, improving carton density and pallet efficiency.
For deeper insights into secondary shipping optimization, read our companion analysis on Blister Card Packaging Logistics and Case-Pack Density.
Card Dimensions Have to Work With the Pack-Out Process
A blister card dieline cannot be engineered solely for marketing appeal; it must integrate seamlessly with fulfillment equipment. Whether a brand packages products in-house or partners with a contract packager, sealing machinery imposes rigid mechanical boundaries.
Heat-sealing equipment—including shuttle sealers, rotary turntables, and continuous carousel lines—relies on dedicated aluminum or composite sealing fixtures (tooling nests). These fixtures hold the blister and card in precise register while heated sealing bars apply uniform downward pressure.
- Tooling Nest Clearances: The card perimeter must match the tooling cavity dimensions with controlled clearance. If the card is cut slightly oversize, it will bind against nest sidewalls, preventing the card from resting flat against the blister flange and causing seal voids.
- Sealing Bar Contact Width: Sealing bars must press evenly across the entire perimeter flange without impinging on the thermoformed blister sidewall.
- Operator Handling & Loading Speed: Excessively tight or awkward card geometries slow down manual loading and automated card pick-and-place feeders, capping assembly throughput.
To align your packaging development with commercial co-packer standards, consult our guide on Blister-Card Packaging and Fulfillment for Co-Packers.
Blister-Card Dimension Strategy Matrix
The following technical matrix provides a comprehensive reference mapping how each dimensional parameter affects structural integrity, retail presentation, and manufacturing operations when under- or over-engineered:
| Dimension / Parameter | Too Small / Under-Engineered | Too Large / Over-Engineered | Optimal Engineering Target |
|---|---|---|---|
| Card Width | Insufficient flange margin, crowded copy, edge seal failure | Reduces retail peg facings across 36"/48" runs, increases substrate cost | Smallest width providing full flange support + planogram density |
| Card Height | Concealed headers when nested on hooks, crowded back instructions | Collides with upper/lower shelf tiers, forces wider peg spacing | Ensures visible header brand zone within vertical shelf clearance |
| Header Area | Weak brand identification, hang slot crowds primary logo | Wastes paperboard, pushes blister downward and distorts hanging center | Balanced billboard establishing brand hierarchy above blister flange |
| Seal / Flange Area | Increases the risk of weak seals, edge lifting, or failure during handling | Consumes card face without adding strength, reduces printable art area | Uniform perimeter margin matched to sealing tooling requirements |
| Substrate Stiffness & Weight | Card bowing, forward curl on pegs, hang-slot tearing under load | Excess packaging weight, elevated board cost with no retail benefit | Structural paperboard weight + vertical grain resisting cantilever load |
| Blister Depth | Crushes product, strains thermoformed plastic, pinches cords/buttons | Excessive forward torque on peg, reduces units per hook, inflates shipping cube | Exact product depth + calibrated clearance for smooth pack-out insertion |
| Cavity Clearance | Binding during insertion, scuffed product finish, flange distortion | Product rattles, slides out of display orientation, visual misalignment | Controlled clearance margin holding item stably in prime display angle |
| Hang-Hole Position | Card hangs crookedly on peg hook, misaligns retail brand block | Weakened upper paperboard edge, increased risk of hook tear-out | Suspension vertex centered directly over composite center of gravity |
| Printed Copy Area | Illegible regulatory text, crowded barcodes risking scanner failures | Excess white space, inflated card footprint with unmonetized paperboard | Clear graphic hierarchy with scannable barcode quiet zones |
| Case-Pack Envelope | Excess master shipper void, inflated freight volume metrics | Shipper exceeds 40"×48" pallet footprint, causes pallet overhang damage | Calibrated dimensional ratios enabling head-to-foot nesting |
Should Every SKU Have Its Own Blister-Card Size?
When a brand manufactures an extensive catalog of products—such as 15 different hand tools or 25 electrical connectors—packaging engineers face an essential strategic choice: Should every SKU receive an individually tailored card size, or should the product line be grouped into standardized card platforms?
Custom Size Per SKU
Pros: Absolute minimum paperboard consumption for each item; perfectly scaled visual framing.
Cons: High tooling tooling costs (unique cutting dies and heat-seal trays for every SKU), fragmented print purchasing volumes, inventory complexity, and uneven retail peg alignment.
Standardized Card Platforms
Pros: Shared heat-seal tooling fixtures, consolidated master shipping cartons, uniform retail brand block on peg fixtures, and massive print economies of scale.
Cons: Smaller SKUs within a platform have slight excess paperboard margin, requiring disciplined graphic balance.
In many retail and contract packaging programs, the operational advantages of card standardization can outweigh minor material savings. By consolidating a larger product line into a few shared card footprints (such as Small, Medium, and Large), brands can often reduce tooling variety, simplify packing-line changeovers, and present a more cohesive visual presentation across retail pegboards. However, the balance between board consumption and operational efficiency should be evaluated for each catalog’s volume and SKU mix.
Card Standardization Can Support Multi-SKU Production (The qikCombo Program)
Standardizing card footprints can also unlock production efficiencies such as qikCombo shared-run combination printing.
In traditional offset card printing, ordering separate small runs for multiple individual blister card designs can involve repeated setups and plate costs for each SKU.
When a brand standardizes related SKUs on a shared card size, multiple card versions can often be combined on shared press sheets. Because the cards share the same paperboard substrate and heat-seal coating formulation, setup and plate overhead can be distributed across the product family, helping brands manage inventory across diverse SKU variations more economically.
Discover how gang printing transforms multi-item retail programs in our guide on High-Volume Blister Cards for Multi-SKU Product Lines.
Retailer-Specific Dimensional Requirements
Retail compliance manuals and merchant routing guides frequently include dimensional and layout requirements for carded merchandise. While exact specifications vary by retailer and category program, guidelines commonly address:
- Maximum Package Width: Width limits designed to ensure adjacent packages on standard peg centers do not crowd or interlock during consumer browsing.
- Hang-Hole Specifications: Preferred hang-hole styles (such as standard euro or delta slots) along with minimum top-edge margin requirements to prevent tear-out.
- Barcode Placement & Quiet Zones: Prescribed placement for UPC/GTIN barcodes, including sufficient clearance from blister flanges and die-cut edges to ensure reliable scanning.
- Security Tag Accommodation: Sufficient card surface or cavity clearance to accommodate EAS or RFID security tags where required without obscuring key product features.
To ensure your package passes retail routing guide audits without chargebacks, review our analysis on High-Volume Blister Cards for Retailer-Specific Programs.
Signs an Existing Blister Card Should Be Resized
Packaging dimensions should never be static. As products evolve, retail fixtures shift, and shipping rates increase, legacy blister cards can become operational liabilities. The following 9 triggers indicate that an existing blister card is overdue for a dimensional engineering redesign:
The Package Tilts or Hangs Crookedly on Display Hooks
The hang hole is centered on the card rather than aligned with the product's actual center of mass, causing the package to skew sideways.
Hang Holes Tear Under Store Handling
Insufficient paperboard margin above the hang slot allows wire peg hooks to rip through the substrate during routine customer browsing.
Cards Bow or Crease Under Product Weight
The card area is too large for its substrate stiffness, or the paperboard grain direction runs horizontally across the load plane.
Required Brand or Technical Information Is Crammed
Important regulatory icons, multi-language instructions, or barcode quiet zones are encroaching on the blister sealing flange.
The Blister Flange Reaches the Extreme Card Edge
Zero margin between the sealing flange and the card border leads to localized heat-seal voids, peeling corners, and transit damage.
Retail Category Buyers Request a Smaller Footprint
Merchant partners demand tighter card widths to fit additional facings or accommodate updated planogram resets.
Master Shipping Cartons Contain Excessive Air
Poor package cubing and lack of nesting capability result in elevated freight volume charges and under-utilized shipping pallets.
Tooling Proliferation Across the Catalog
Every SKU utilizes an idiosyncratic card size, forcing co-packers to maintain dozens of separate sealing trays and die sets.
An Updated Product Revision No Longer Fits Smoothly
Minor product updates (such as an added wire, grip texture, or accessory) cause binding, pinched components, or cracked blister sidewalls.
PM Packaging's Custom Blister Engineering Capabilities
PM Packaging works with brand owners and contract packagers to evaluate blister cards, thermoformed cavities, and master shipping configurations together. By aligning card dielines, substrate caliper, heat-seal coating, and pack-out requirements early in development, we help packaging teams avoid dimensional conflicts before tooling and production begin.
Our commercial blister packaging support includes:
CAD Dieline & Prototype Engineering
Precision structural design calculating center-of-gravity balance, flange margins, and grain orientation using production CAD tools and physical sample cutting.
Custom Thermoform Cavity Tooling
In-house tooling design for custom plastic blister pockets engineered with tailored insertion clearances and orientation locking detents.
High-Speed Sheetfed Offset Printing
Vibrant multi-color process and spot printing on premium solid bleached sulfate paperboard with advanced color management.
Inline High-Tack Heat-Seal Coating
Precision application of high-performance heat-seal coatings calibrated for clean, fibre-tearing seal bonds with PVC and RPET blisters.
Versatile Card Formats
Complete structural support for face-seal cards, two-piece fold-over cards, and trapped blister configurations.
qikCombo Multi-SKU Cost Optimization
Shared-run manufacturing programs that combine multiple standardized SKU designs onto shared press sheets to minimize plate and setup costs.
Learn more about our comprehensive blister packaging capabilities on our dedicated service overview for Custom Blister Cards.
What to Provide for a Blister-Card Dimensional Review
If you are developing a new retail product line or auditing an existing blister card catalog to optimize pack-out and shipping costs, providing the following 10 data points enables our structural engineering team to produce an optimized dieline recommendation:
The Pre-RFQ Dimensional Intake Checklist
- Physical Product Samples or 3D CAD Files: Accurate physical units or STEP/IGES files showing exact dimensions, contours, and potential protrusions.
- Weight & Mass Distribution: Item weight and whether the center of gravity is centered or significantly offset.
- Retail Fixture Environment: Standard pegboard hook, double-wire prong, slatwall, sidekick, or counter PDQ display tray.
- Planogram Dimensional Constraints: Maximum allowable width and height permitted by your primary retail category buyer.
- Graphic & Regulatory Copy Requirements: Scope of required branding, product claims, multi-language copy, UPC barcodes, and warnings.
- Catalog SKU Count & Volume Forecasts: Total number of distinct SKUs in the product family and estimated annual volume per SKU.
- Preferred Packaging Architecture: Face-seal blister, fold-over card, or trapped blister format.
- Fulfillment & Pack-Out Method: In-house rotary heat sealer, manual shuttle sealer, automated carousel, or external contract packager.
- Target Master Carton Pack-Out: Desired inner-pack and master shipper counts (e.g., 6, 12, or 24 units per carton).
- Palletization & Warehouse Requirements: Standard 40 × 48-inch North American pallet limits, maximum stacking heights, and distribution requirements.
Frequently Asked Questions: Blister Card Sizing & Dimensions
How do you determine the correct size for a blister card?
The correct size is calculated by combining the product dimensions, necessary cavity clearance tolerances, sealing flange contact width, upper header billboard space, hang-hole paperboard margins, and retail planogram constraints. The objective is the smallest disciplined footprint that fulfills all structural, graphic, and merchandising requirements.
How much space should be left around a blister cavity?
Sufficient margin must be preserved between the cavity pocket and the outer card edge to accommodate an unbroken sealing flange plus structural border margins. This ensures heat-sealing tooling fixtures make full contact with the flange without impinging on the card edge or blister sidewalls.
Does blister-card size affect seal performance?
Yes. Sizing a card too tightly to the blister cavity forces the flange dangerously close to the cut edge, leaving inadequate surface area for uniform heat-sealing pressure. This leads to edge lifting and premature seal separation. A properly proportioned card provides a stable backing substrate for robust seal bonding.
How does card width affect retail peg density?
Card width directly dictates how many peg hook facings fit across a retail shelf section. For example, on a 36-inch pegboard section with typical hook clearances, moving from a 4-inch wide card to a 5-inch wide card can reduce total facings from roughly 8 columns to 6, significantly reducing product presence.
How does blister depth affect case-pack efficiency?
Cavity depth directly influences master carton volume. Unnecessary depth adds void space to shipping cases and inflates volumetric freight charges. Where card proportions allow alternating head-to-foot nesting, cavities can nest against adjacent flat card headers, materially reducing unused void space in the master carton.
Can several SKUs share the same blister-card size?
Yes. Grouping related SKUs into standardized card platforms (such as Small, Medium, and Large) can consolidate heat-seal tooling fixtures, create a uniform brand block on retail fixtures, and allow brands to take advantage of shared-run combination printing programs like qikCombo.
Does product weight affect blister-card dimensions?
Product weight influences the required substrate stiffness, paperboard weight, and grain direction rather than just surface area. Heavier products require vertical grain alignment and sufficient paperboard margin above the hang hole to prevent hook tear-out and forward card bowing.
When should an existing blister card be resized?
Common indicators include packages hanging crookedly on peg hooks, cards bowing forward under product weight, torn hang slots, crammed graphic copy, edge flange lifting, retailer requests for higher facing density, or excessive empty space in master shipping cartons.